Hey everyone, it’s Jake here, from that carrier tape materials supplier you’ve probably chatted with before—you know, the one that’s not afraid to answer last-minute questions about tape specs at 9 PM. Today I wanna dive into something that’s been popping up in our DMs non-stop lately: surface roughness for carrier tape materials. Like, I get it—when you’re shipping tiny SMD resistors or delicate ICs, it’s easy to brush roughness off as some random lab number. But trust me, skip this and you’re gonna be fielding a whole lot of “wait, our parts got scratched” or “feed rates are jittery” calls, and no one needs that. Let’s break this down, no overly technical jargon (okay, maybe a little, but I’ll explain it like we’re geeking out over a new tool in our workshop). Carrier Tape Materials
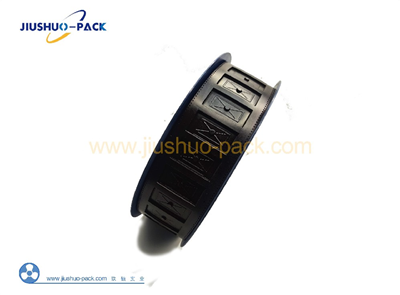
First, let’s keep it real—what even is surface roughness, when we’re talking carrier tape? You’ve got Ra, Rz, Rq, right? Let’s define ‘em quick, no textbook stuff: Ra is the average height of the bumps and valleys on the tape surface, measured in micrometers (μm) for us—so smaller = smoother, like when you run your finger over a glass vs. a sanded table. Rz is the average height difference between the tallest peak and deepest valley in a single spot, and Rq is the root mean square, basically a more sensitive version of Ra for the really tiny irregularities.
Now, why does this matter more than just how the tape looks? Let’s start with the big one: part damage. Carrier tape’s whole job is to cradle tiny electronic parts—think 0201 resistors, even smaller 01005 these days, or fragile fine-pitch ICs. If the inner surface (the part that touches the parts!) is too rough? Those tiny bumps act like little sandpaper grit. When the tape moves through a pick-and-place machine, the parts slide back and forth, and boom—scratched resistor terminations, chipped IC pins, maybe even a tiny scratch that messes up a component’s electrical performance even if you can’t see it. We’ve had a customer come to us after switching to a cheaper tape from a random supplier, and they had a 12% failure rate on scratch-sensitive ICs. Switched to our tape with the right roughness, that dropped to 0.02%. Not a stat I made up—we tracked that for 3 months, so you know it’s real.
Next up: machine compatibility. Pick-and-place machines aren’t just pushing tape around—they rely on consistent feed friction, and smooth inner surfaces mean consistent part movement. If roughness is all over the place (like if a supplier cuts corners on their polishing process), some spots have high friction, some low. The feed mechanism starts skipping, parts don’t align right, maybe even get stuck mid-feed. We’ve had a newbie operator at a customer plant call us panicking because their pick-and-place was throwing 2 parts a minute—turned out the old tape had Ra ranging from 0.8μm to 2.1μm across a single roll. We sent them a sample of our standard tape, same Ra ±0.1μm, and that feed error was gone by the end of their shift. Worth noting, too: newer high-speed SMT lines (the ones pumping out 100k parts an hour) are way pickier about this than older, slower machines. If you’re running an 8-line plant, skips add up to hundreds of thousands of bad boards a week—roughness isn’t a trivial detail here.
Wait, let’s split this into actual requirements, because “smooth” is vague. First, distinguish between inner surface (part contact) and outer surface (the top of the tape, where the cover tape seals to it). Outer roughness is less critical for part damage, but if it’s too rough, the cover tape seal gets weak—air or moisture gets in, or the cover tape peels too hard when picking, which can yank parts out of pockets. We usually recommend outer Ra ≤ 1.2μm, inner Ra ≤ 0.8μm for standard SMT parts. But wait, there are exceptions! If you’re working with ultra-delicate parts, like MEMS sensors or thin-film capacitors? We bump that inner Ra down to ≤ 0.5μm. And for parts that are a little sturdier, like through-hole adapters or larger resistors, inner Ra can go up to 1.0μm—no need to pay for extra smoothness you don’t need, that’s a waste of money. A lot of suppliers will push you to get the lowest Ra possible for everything, but that’s just gouging you—we’re not like that.
Now, what about when a supplier cuts corners here? How can you tell if your tape is actually meeting these specs? We see two main issues from cheap suppliers: first, inconsistent roughness across a roll. They might run a batch through a polisher for 2 seconds instead of 10, so the start of the roll is Ra 0.7μm, the end is 1.8μm. Second, rough edges around the pockets. When you punch the pockets into the carrier tape, you get a tiny burr on the inner edge. If that burr is left, it scratches parts as they’re loaded or unloaded. We always do a secondary deburr pass on our pockets, and measure edge roughness separately—we keep that edge Ra ≤ 1.0μm, even if the main inner surface is lower. A lot of suppliers skip that step, and you’d be shocked how many part scratches are actually from pocket edges, not the flat inner surface.
Also, material type plays a role here! Wait, we work with multiple materials—standard polystyrene (PS), high-temperature polycarbonate (PC), static-dissipative (ESD) compounds for sensitive stuff. PS is cheaper, easier to get smooth, so its roughness specs are straightforward. PC is stiffer, used for high-heat reflow applications, so it’s a little trickier to polish evenly—our PC tape has a slightly higher Ra tolerance, usually ±0.15μm vs. PS’s ±0.1μm, because PC just doesn’t polish as consistently. And ESD materials? We make sure all our ESD compounds don’t have any filler clumps, which would create random high roughness spots—so we do extra mixing and filtering steps, which is why our ESD tape costs a little more, but it’s worth it for no clumps messing up roughness.
Wait, let’s talk about a common myth I hear all the time: “Cover tape will protect the inner surface, so roughness doesn’t matter.” No, dude. When you’re loading the tape into the machine, you peel back the cover tape. As you peel it, parts slide a tiny bit, and any roughness on the inner surface is right there to scratch them. Even if the cover tape is on, when the tape is being transported, it rubs against adjacent rolls or guides in the machine—rough outer surface causes friction, which can leave marks on the outer layer, and if outer roughness is too high, it can even transfer to the inner surface over time. So that myth is totally debunked—roughness matters no matter what.
Now, let’s get practical: what should you actually ask your current carrier tape supplier, or when ordering new tape? Don’t just say “give me smooth tape.” Ask for:
- The exact Ra (or Rz, if you prefer) value for inner and outer surfaces, with a tolerance (we give a ±0.1μm tolerance for inner Ra, that’s non-negotiable for us)
- Whether they test pocket edge roughness separately
- What their process is for maintaining consistent roughness across an entire roll (we test every 100 meters, no exceptions—no skipping spots)
- If they offer custom roughness for super sensitive parts (we do, no hassle, just send specs)
We had a customer last month who was having issues with LED parts getting scratched. They thought it was a machine setting, tried 3 different machine techs, tried switching part feed rates, nothing worked. They reached out to us, we asked for their tape specs, looked at their current supplier’s specs—turns out their tape had inner Ra of 1.5μm, way over our recommendation of ≤0.8μm. Sent them our standard LED-specific tape, and they called us 2 days later saying the scratch rate was zero. That’s the stuff that makes our job worth it.
Another thing: testing roughness yourself. You don’t need a $10k lab machine to check. A lot of quality control teams use a surface roughness comparator kit—they’re like $200, portable, easy to use. Run a few spots on the tape, and you can see if it matches the spec. If your current supplier won’t give you a roughness test report when you ask, that’s a red flag. We send a test slip with every single roll, no request needed. Period.
Wait, what about when reflow temperatures are higher? Like, for automotive parts that need to go through lead-free reflow at 260°C? The material can soften a little, right? If the inner surface was rough at room temp, when it heats up, those tiny bumps can get even more pronounced, because the material flows a tiny bit. That’s a big one for automotive and aerospace customers, who have way higher reliability standards. Our high-temperature PC tape is formulated to keep roughness consistent at high temps, so we only recommend it for those applications, and we test roughness before and after reflow to make sure it doesn’t jump. A lot of cheap suppliers don’t do that post-reflow test, so their tape seems fine at room temp, but after reflow, it’s too rough.
Let’s wrap this up, no fancy stuff. Surface roughness isn’t just a random metric—it’s tied to part yield, machine uptime, and less stress in your SMT plant. The requirements aren’t one-size-fits-all, either—standard parts need inner Ra ≤0.8μm, ultra-delicate parts ≤0.5μm, outer ≤1.2μm, pocket edges ≤1.0μm, adjusted slightly for the material you’re using. And always work with a supplier that’s transparent about their roughness specs, tests consistently, and doesn’t cut corners.
If you’re tired of part scratches, feed errors, or supplier ghosting when you ask for test reports, hit us up to chat about your carrier tape needs. We can send free samples, walk you through our roughness test data, no hard sell—just honest answers. We’ve worked with SMT plants of all sizes, from 2-line startups to big automotive facilities, and we know how to get the roughness right for your specific parts, no guesswork.
Paper Carrier Tape References:
- SMT Magazine. (2022). "Surface Roughness Impacts on Carrier Tape Performance for Fine-Pitch Components." Vol. 38, No. 4, pp. 45-52.
- IPC-A-500. (2021). "Specification for Carrier Tapes for Surface Mount Devices." Association Connecting Electronics Industries.
- Electronic Components and Technology Conference (ECTC). (2020). "The Effect of Carrier Tape Surface Roughness on Microelectronic Component Reliability." Proceedings of the 70th ECTC, pp. 1892-1897.
- Plastics Engineering. (2019). "Surface Finish Requirements for Polymer Carrier Tapes in High-Speed SMT Applications." Vol. 75, No. 6, pp. 22-27.
Dongguan Jiushuo Industrial Co., Ltd.
As one of the most professional carrier tape materials manufacturers and suppliers in China, we also support customized service. Please feel free to buy high quality carrier tape materials made in China here from our factory. Contact us for more details.
Address: 11th Floor, Building 2, Chuangfu Center, Chashan Town, Dongguan City, Guangdong Province, China
E-mail: sales06@zaidaiw.com
WebSite: https://www.carriertape-pack.com/
