Hey there! If you’re deep into zinc die casting (or just dipping your toes into learning about it), you’ve probably heard the term “gating system” thrown around. At our zinc die casting shop, it’s one of the first things I walk new clients through—because get this: a bad gating system can turn even a perfectly good zinc alloy part into a reject, and a good one? It cuts down on defects, speeds up cycle times, and saves you a ton of cash. Today, I wanna break this down like I would for a guy who just emailed asking, “Wait, what even IS a gating system, and why should I care?” Zinc Die Casting
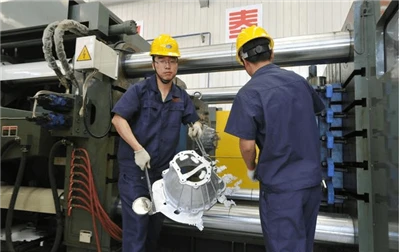
First off, let’s keep it simple. The gating system is basically the “plumbing” of a die casting mold. It’s the whole network of channels that molten zinc flows through to get from the machine’s shot chamber into the actual mold cavity where your part takes shape. If you’ve ever poured water through a funnel into a narrow bottle, that’s the same idea—except with way higher stakes, because we’re talking molten zinc at like 380-420°C, moving at 30-60 meters per second, and any misstep leads to cold shuts, porosity, or even the whole part getting stuck in the die.
Let’s pull back the curtain and talk about the parts that make up this system, because every single one matters. No skipping these—trust me, I’ve seen interns mess up the runner size once and cost us a whole day of scrapped parts. First up is the sprue: that’s the main vertical channel that feeds the shot machine’s nozzle. It’s tapered on purpose—wider at the bottom, narrower at the top—so that molten zinc doesn’t get trapped as it flows down. Next is the runner system: that’s the network of horizontal (or sometimes angled) channels that branch off the sprue to deliver metal to each mold cavity. Then there’s the gate itself: that’s the tiny, precise opening where metal finally dumps into the part cavity. It’s usually super thin, because we want that focused, high-speed flow to fill the cavity before any part of the zinc starts to cool. And last (you can’t forget this) is the overflow system: these little pockets and channels that sit at the end of the flow path, catching the first, dirty bit of zinc (it has oxides, air bubbles, whatever) that would otherwise end up in your good part.
Wait, why is zinc different from aluminum or brass here? Good question. Zinc has a lower melting point, right? It’s way more fluid when molten, which sounds like a win—but that means it fills cavities faster, but it also cools faster too. So the gating system for zinc isn’t one-size-fits-all. If you’re making a tiny, intricate part (like a connector pin or a watch case), you need a gate that’s smaller, more focused, so it doesn’t spread out and cool before filling every little groove. If you’re making a larger part, say a housing for a power tool, you need a runner that’s the right diameter—too small, and the metal slows down, gets cold, and leaves a cold shut (that’s a line where two streams of zinc didn’t fuse together); too big, and you’re wasting alloy, plus the gate can be a pain to trim later.
Let’s talk common mistakes I see clients make, too. A lot of guys new to die casting think, “More flow = better,” so they make the runners way too big. Nope. That leads to what we call “air entrainment”—when fast-moving metal hits a wide channel and slams into air, trapping tiny bubbles inside. Those bubbles turn into porosity, which makes the part weak, or causes it to leak if it’s for a fluid component. Another mistake is skipping the overflow system. I had a client once who refused to let us add overflows because he “didn’t want extra material to trim.” The first production run had 18% reject rate—all from surface oxides trapped in the part. Adding overflows cut that to 1% overnight. Worth every extra 10 minutes of trimming, trust me.
At our shop, we don’t just pull a gating design off a shelf. Every job is custom. We start with the part geometry first. If it’s a part with thin walls, like a laptop hinge, we need a gating system that directs metal to the thickest sections first, so those areas stay hot longer and fill properly. If it’s a part with deep, narrow holes, we’ll sometimes add multiple gates (called “multi-gating”) so the flow doesn’t have to travel too far. We also factor in the zinc alloy grade—ZAMAK 3 is our go-to for most jobs, but ZAMAK 5 is for higher strength, and ZAMAK 7 is for decorative parts that get plated. Each alloy has slightly different fluidity, so the gate size and runner length shift a little.
We even test gating designs before we cut steel for the mold. A lot of guys skip this step and end up stuck with a bad mold that costs thousands to fix. We use simulation software—nothing fancy, just standard die casting flow sim—to run a virtual pour, see where the metal fills fast, where it might get trapped, if there’s going to be porosity, and adjust the gating before we even touch the mill. Last quarter, we did a job for a medical device client that had 12 tiny cavities. The simulation caught a spot where two runners would cross, creating a flow bottleneck. We fixed it before machining, and the first sample run was 100% good. Saved us 2 days of rework, and the client loved how fast we turned it around.
Now, you might be thinking, “Okay, that makes sense, but does it really matter for my part?” Let’s take real examples from our shop. A few months back, we had a client making door handles for a commercial building. They were using aluminum die casting before, but switched to zinc because it’s more corrosion-resistant and takes a nicer finish. Their first gating design was copied from an aluminum part—runner sizes way too big, gate in the wrong spot. The parts came out with weird surface blemishes, and some wouldn’t fit the mounting holes because of shrinkage. We reworked the gating: moved the gate to a thick section at the base of the handle, shrunk the runner diameter, added overflows at the ends of the part where air would get trapped. Next sample run: no blemishes, perfect mounting holes, and the strength was exactly what they needed. They ended up sending us 5 more different door handle models after that.
Another example: a consumer electronics client making wireless earbud cases. Tiny, super intricate, thin walls—any defect would ruin the part. Their initial design had a single gate in the center, but the simulation showed the metal would flow too fast and create turbulence, leaving micro-porosity that would cause the finish to peel when plated. We switched to two gates, one on each side of the case, so the metal flowed in evenly, no turbulence. The first plated batch was 0 defects. They now use that gating setup on all their small earbud and headphone accessories.

So, to wrap this up (and keep it real, no jargon overload): the gating system isn’t just a technical detail—it’s make or break for your zinc die cast part. It affects everything from surface finish and strength to how much scrap you have and how fast you get your parts. At our zinc die casting shop, we treat every gating design like it’s our own job, because we know that when our clients win, we win too.
Magnesium Die Casting If you’re currently struggling with bad parts, high scrap rates, or just want to optimize your next zinc die casting project, I’m here to help. We don’t do one-size-fits-all solutions, and we’ll walk you through every part of the process, including the gating system, so you know exactly what’s going into your parts. Hit me up, tell me about your project, and we can talk through how to make it work right.
References
- Kennedy, R. (2020). Zinc Die Casting: Design, Process, and Applications. Industrial Press.
- Semiatin, S. L. (Ed.). (2013). Metal Powder Industries Federation: Die Casting Handbook (4th ed.). Metal Powder Industries Federation.
- Johnsen, T. (2018). Gating System Design for Non-Ferrous Die Casting. Journal of Die Casting Technology, 12(2), 45-52.
Shenzhen Shunhaoda Technology Co., Ltd.
With abundant experience, we are one of the most professional zinc die casting manufacturers and suppliers in China. If you’re going to buy bulk high quality zinc die casting made in China, welcome to get free sample from our factory. Also, custom service is available.
Address: 902, Building A3, Tianrui Industrial Park, No. 35 Fuyuan 1st Road, Zhancheng Community, Fuhai Street, Bao’an District, Shenzhen
E-mail: sales@shdindustry.com
WebSite: https://www.shd-industry.com/
