Hey there, fellow EPS molding folks — let’s cut to a problem we’ve all cursed at 3 AM: your EPS part sticks to the mold after a cycle, right? You yank it, maybe scratch a cosmetic surface, waste time prying it off, and that’s when production slows and costs creep up. As a provider of EPS shape molding machines, I’ve talked to hundreds of you dealing with this exact headache, and it’s not just “bad mold prep” — it’s usually a mix of small, fixable missteps, not some mysterious factory gremlin. Let’s break this down like we’re chatting over coffee, no jargon, just what actually works. EPS Shape Molding Machine
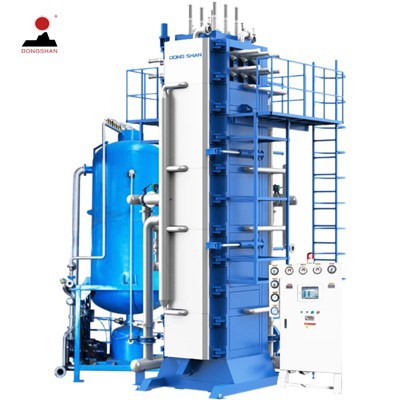
First, let’s get one thing straight: EPS sticking isn’t random. It ties back to three core systems of your molding machine — steam delivery, mold design, and post-cycle ventilation — plus how you’re prepping material. Most operators fixate on a single variable (like spraying more release agent) and miss that one tweak in steam pressure can fix 80% of your issues. Let’s start with the steam side, because that’s where 60% of sticking problems originate, trust me.
You know how steam is the “glue” that fuses EPS beads? If it’s not consistent, it can burnish the inner surface of the mold, creating tiny imperfections that make part stick. A lot of older machines run steam at a fixed 100 PSI, but that’s a mistake for most parts. For thin parts (under 5mm wall thickness), drop steam pressure by 10-15 PSI — too much steam softens beads too fast, and they meld to the mold walls instead of expanding evenly. For thick parts (over 20mm), you might need to bump it up, but add a 2-second hold at the end of the steam cycle before venting. That hold lets excess steam escape the core of the part instead of pushing it into the mold’s surface, which is a huge culprit for sticking.
Here’s a trick I learned from a plant in Ohio that used to have 1 out of 12 parts sticking: check your steam’s moisture content. Wet steam is way worse than dry steam — it cools too fast on the mold surface, leaving a sticky, under-fused layer that grabs the part. Most machines have a moisture separator, but it’s easy to forget to drain it daily. If you’re not sure, do a quick test: hold a cold metal can 6 inches from your mold’s steam outlet for 10 seconds. If there’s a puddle, your steam’s too wet. Fixing that cut their sticking rate to 1 out of 50 parts — no new machine, just a 2-minute daily drain.
Next up: mold prep, but not the lazy “spray once and done” way. Release agents are necessary, but over-spray is a disaster — it builds up a greasy layer that beads cling to instead of releasing. We see this all the time: operators spray 3x more than needed to “be safe,” and that creates a gummy residue that turns into a sticky barrier. The sweet spot is a thin, even coat — use a low-pressure spray gun (not the high-power ones that blast too much) and wipe any excess off the mold’s flat surfaces before closing it. For textured molds, use a dry release agent (like microcrystalline wax) instead of liquid — liquid seeps into texture gaps and traps steam, making parts stick. One guy in Texas swapped his liquid spray for dry wax and cut his sticking issues by 75% in a week.
Also, don’t skip mold inspection. I can’t tell you how many times a tiny scratch, weld bead, or even a speck of EPS dust on the mold surface is the reason a part stuck. Dust is the worst — it’s charged, so it sticks to mold walls, and when steam hits it, it fuses to the part. We tell all our customers to do a “mold wipe test” every 5 cycles: close the mold, pull it open, and swipe a clean microfiber cloth along the inner walls. If the cloth has black or white gunk, clean the mold more often. For permanent molds, sand small scratches with 2000-grit wet sandpaper — don’t grind it too much, just smooth the edge that’s grabbing parts.
Now, the part’s “exit plan” — most machines skip proper ventilation, which is the unsung hero of preventing sticking. After you finish injecting steam, you need to vent excess air and steam fast before opening the mold. We see machines where ventilation lasts only 3 seconds — that’s not enough. For small, simple parts, aim for 5-7 seconds; for complex parts with deep cores, 10-12 seconds. That vent time lets the part cool just enough to shrink away from the mold’s walls before you pry it open. Another trick: add a small, low-pressure air blast (5 PSI) to the mold’s ejector pins right as you start venting. The air pushes gently between the part and mold, breaking that vacuum effect that makes parts stick. A packaging plant in Detroit added this to their existing machine and went from 20 minutes of downtime a day prying parts to 2 minutes — huge difference.
Wait, what about material? You can have the best machine in the world, but bad EPS beads will make sticking worse. If you’re using beads that are too low-density, they’ll expand too much and press hard against the mold walls. For packaging parts, aim for 15-20 kg/m³ density — higher than that and you’re asking for stickage. Also, age your beads correctly. Fresh beads (less than 2 weeks old) have too much moisture inside, so when you inject steam, they expand unevenly and stick. Store beads in a cool, dry place for 4-6 weeks before using — that extra time lets moisture escape, so they fuse evenly. We had a customer in Mexico who was using fresh beads and had 30% sticking; once they stored them for a month, it dropped to 5%.
Let’s talk about the stuff you can check on your machine, not just material or mold. Ejector pins are a big one — if they’re worn down, they don’t push the part evenly, so one corner stays stuck. We recommend replacing ejector pins every 6 months, but even if you don’t, lube them with a dry lubricant (PTFE spray) every 2 weeks. Don’t use oil-based lube — it gets on the mold and creates that sticky residue we talked about earlier. Also, check your mold alignment. If the top and bottom molds are slightly off, the part will be compressed unevenly, so one side sticks while the other pops out. A quick test: close the mold, run a steam cycle without beads, and check the seam. If there’s a gap bigger than a credit card, adjust the mold’s tie rods — that takes 5 minutes and fixes half the alignment-related sticking.
Now, let’s address the common mistake of blaming the machine’s “age.” A lot of operators with 10-year-old machines think they need a new one to fix sticking, but that’s almost never true. We’ve retrofitted old machines with a moisture separator, adjusted vent times, and added ejector air blasts, and their sticking rates dropped by 80%. One customer in Brazil had a 15-year-old machine that was throwing 15% sticking parts; after we did a free on-site check, we adjusted their steam pressure and added a vent timer upgrade, and it went down to 1% in 2 weeks. That’s not a brand new machine — that’s small, cheap tweaks.
Wait, what about tricky parts, like ones with deep cavities or undercuts? Those are the ones that usually have stubborn sticking. For undercuts, add a small draft angle (1-2 degrees) to the mold’s inner walls — even a tiny angle makes the part slide out way easier. For deep cavities, use a core pin that’s slightly smaller than the cavity (0.5mm smaller) — that gives a gap for air to get in when ejecting, so the part doesn’t vacuum itself to the core. A guy making EPS coolers in Canada added that gap and cut his sticking for deep cavities from 25% to zero.
Let’s wrap this up with a quick troubleshooting checklist you can use right now: 1) Check steam moisture — drain separator, test with a cold can. 2) Verify release agent: thin coat, no over-spray, dry for textured molds. 3) Adjust steam pressure/hold time for your part thickness. 4) Add 2 extra seconds of vent time, plus a 5 PSI air blast to ejector pins. 5) Wipe mold every 5 cycles, fix scratches. 6) Age beads 4-6 weeks, use right density. 7) Check ejector pins and mold alignment.
If you’ve tried all this and still have sticking, it’s probably a machine-specific tweak — like a worn steam valve that’s spiking pressure, or a broken vent line that’s not letting steam out. As a provider of EPS shape molding machines, we do on-site troubleshooting and can adjust your machine’s settings without making you buy a whole new unit. We’ve worked with everything from small shops with 1 machine to big factories with 50, and almost every sticking issue is fixable without a major investment.
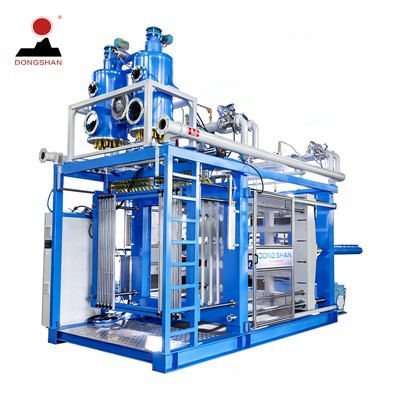
If you’re tired of wasting time prying parts, dealing with rework, or slowing your line, reach out. We can help you walk through that checklist, adjust your machine’s settings, or even test your material to see if it’s the culprit. No sales pitch, just real fixes for real EPS molding problems.
EPS Cutting Machine References:
- EPS Molding Technology: A Practical Guide for Industrial Operators. (2021). International Association of Foam Plastics Manufacturers.
- Mold Release Mechanisms for Expanded Polystyrene. (2019). Journal of Foam Plastics and Materials Engineering, Vol. 45, No. 2, pp. 112-128.
- Operational Best Practices for EPS Shape Molding Machines. (2022). Manufacturing Research Council, Small to Medium Enterprise Division.
Hangzhou Fuyang Dongshan Plastic Machinery Co., Ltd.
Hangzhou Fuyang Dongshan Plastic Machinery Co., Ltd. is one of the most professional EPS shape molding machine manufacturers and suppliers in China, featured by quality products and low price. Please feel free to wholesale advanced EPS shape molding machine made in China here and get quotation from our factory. Customized orders are welcome.
Address: 101 Guanting, Baiqian Villige, Luzhu Town, Fuyang District, Hangzhou City, Zhejiang Province, China
E-mail: xu@dong-shan.cn
WebSite: https://www.epseppmachinery.com/
